Bonding method: start from material and strength
Solvent bonding (cyclohexanone / tetrahydrofuran)
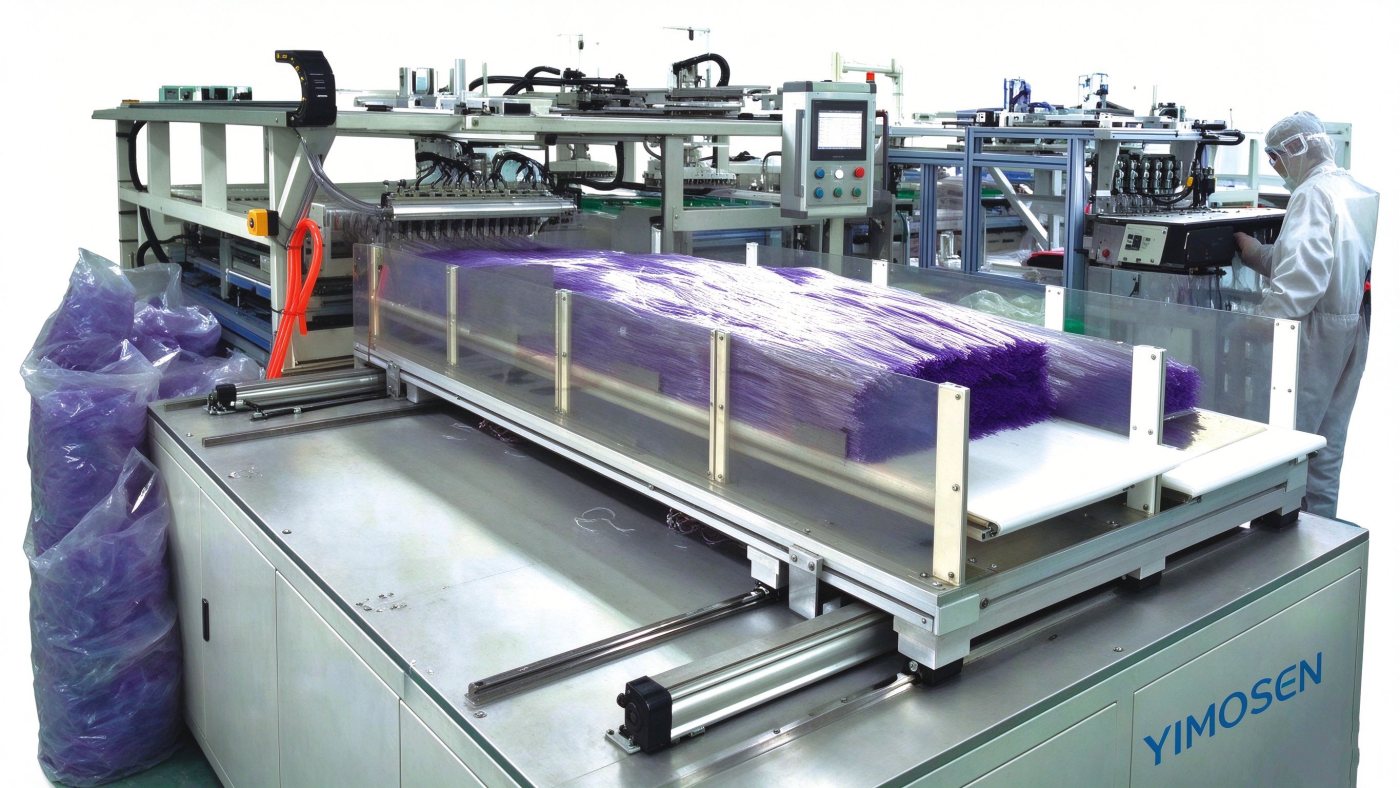
The nasal cannula branch assembly machine and the nasal cannula main catheter assembly machine use cyclohexanone or tetrahydrofuran at the catheter bonding points. The catheter adopts an external adhesive coating method for uniform, firm bonding, with end-face assembly error of ±0.5mm.
UV adhesive with UV light curing
High-pressure syringe pump extension tubes have to withstand higher pressure. Their assembly machine bonds the outer cone joint, inner cone joint, one-way valve, conduit and joint protective cap, using UV adhesive cured by a UV light source, with leak detection and defective dosing identification.
Tightness testing: the quality gate for tube products
The nasal cannula main catheter assembly machine and the extension tube automation equipment both include leak detection. The infusion set assembly machine goes further: a fully automatic online testing system uses air pressure to check whether the assembled product is qualified, and unqualified parts are rejected automatically.
Output reference
- Nasal cannula branch assembly machine: 2,000 sets/hour (four stations)
- Nasal cannula main catheter assembly machine: 4,500 sets/hour, conduit length 1,500-2,100mm
- Extension tube automation equipment: 4,500 sets/hour, conduit length 2,100mm
- Suction tube automation equipment: 4,500 sets/hour with end chamfering, punching, bonding and joint assembly
- Infusion set packaging machine: 5,000 sets/hour
Common questions
Can one machine handle several conduit lengths? The nasal cannula main catheter assembly machine covers 1,500-2,100mm and the extension tube automation equipment covers 2,100mm. Outside that range the tooling has to be adjusted, which can be confirmed during machine selection.